End-of-Line Packaging Automation Guide: Integrating Carton Erectors, Top Seal Tray Sealers, Date Coders, Vision Inspection & Palletizers
What Machines Make Up an End-of-Line Packaging Automation System, and How Should You Synchronize Top Seal Tray Sealers, Carton Erectors, Date Coders, Vision Cameras & Palletizers Without Bottlenecks?
An integrated End-of-Line Packaging Automation system unites 5 core stations: an Automatic Top Seal Tray Sealer, an Automatic Carton Erector (Case Erector) and Case Sealer, Cobot pick-and-place packing, FASTJET date coders paired with HIKROBOT vision inspection, and a Robot Palletizer. To eliminate bottlenecks, engineer downstream stations with a 15–25% speed buffer, accumulation conveyors, and PLC interlock handshakes delivered turnkey by Better Code Co., Ltd.
5-Station Turnkey End-of-Line Packaging Matrix: Architecture, Equipment & PLC Handshakes
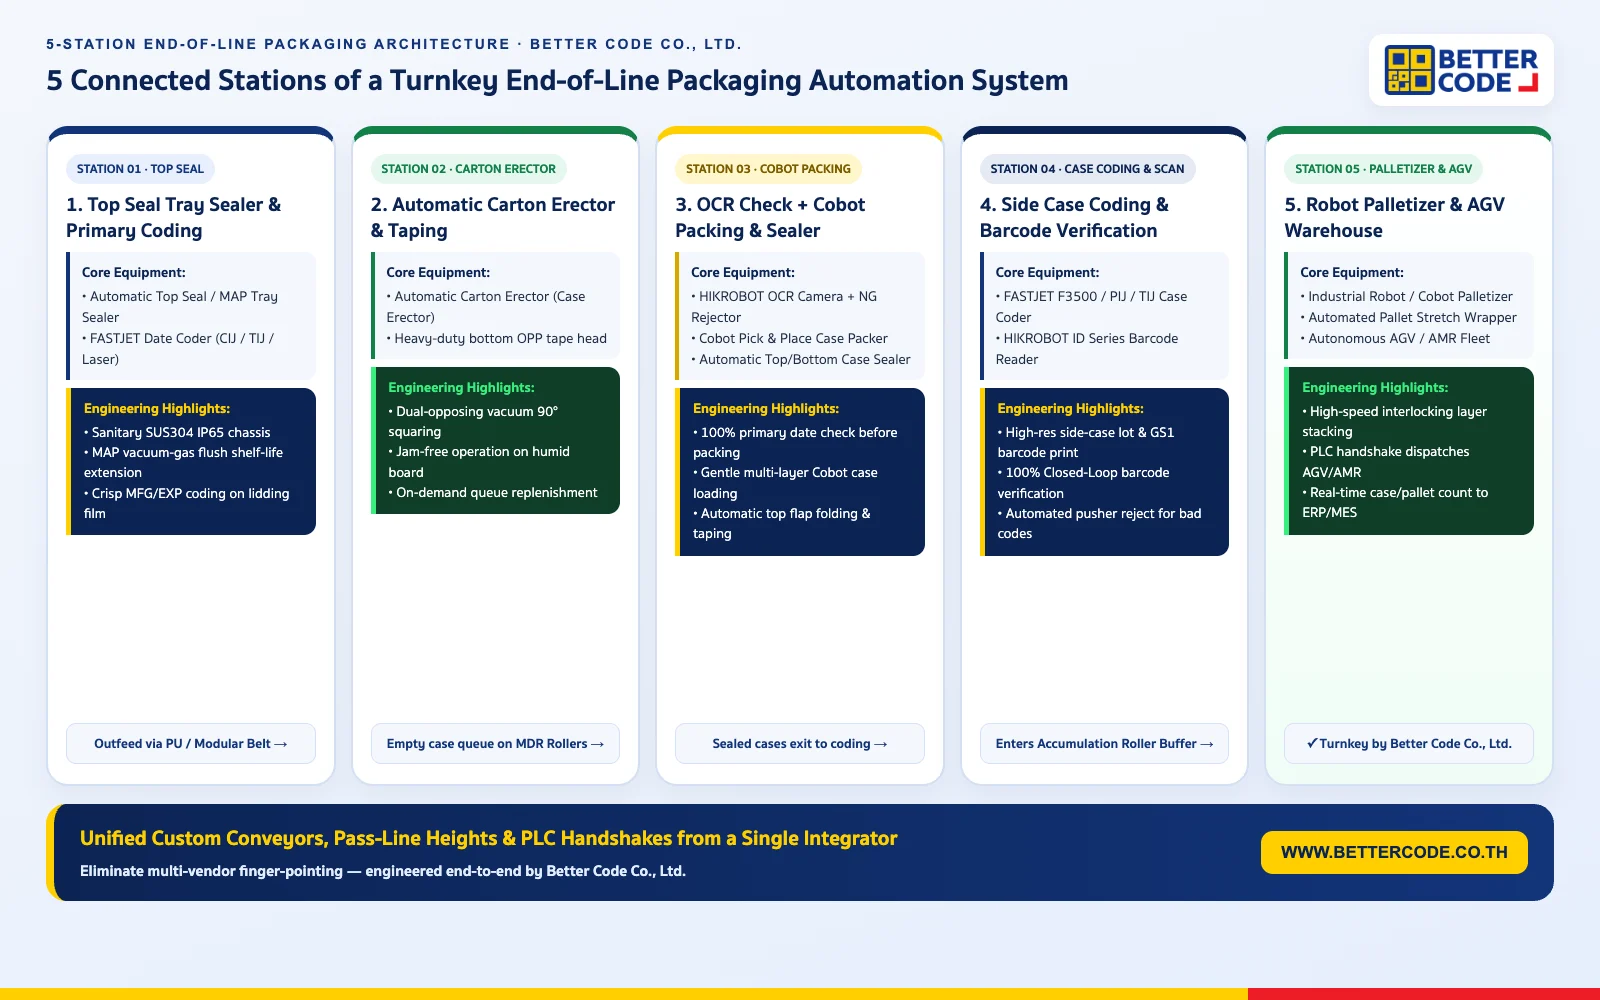
Designing a high-OEE Factory Automation and End-of-Line Packaging system requires synchronizing mechanical pass-line heights, conveyor speeds, and digital quality gates across 5 connected stations. The engineering matrix below details the equipment, conveyor selection, and PLC handshakes for each station:
| End-of-Line Station | 1. Core Machinery | 2. Primary Engineering Function | 3. Inter-Station Conveyor Type | 4. Inline Coding & Vision Verification | 5. PLC Handshake & Interlock Logic |
|---|---|---|---|---|---|
| Station 1: Primary Tray Sealing & Date Coding (Top Seal / MAP + Primary Coder) | Automatic Top Seal / MAP Tray Sealer + FASTJET CIJ / TIJ / Laser Date Coder | Indexes food trays into sealing tooling, executes vacuum & Modified Atmosphere Packaging (MAP) gas flushing, heat-seals & die-cuts barrier film, and prints MFG/EXP/Lot codes | Sanitary SUS304 Modular Belt or FDA PU Flat Belt Conveyor (IP65 washdown rated) with spring-loaded Shaft Encoder | High-contrast non-contact printing of MFG/EXP dates, batch numbers, and 2D QR codes directly onto lidding film or tray rims | Exchanges Tray Indexed / Film Print Trigger pulses and modulates cycle speed upon receiving Downstream Buffer High signals |
| Station 2: Automatic Carton Erecting & Bottom Taping (Case Erector & Case Sealer) | Automatic Carton Erector (Case Erector) and downstream Automatic Case Sealer | Draws flat corrugated blanks from a powered magazine, squares cases to 90° using dual opposing vacuum frames, folds bottom flaps, and applies bottom OPP tape | Motorized Driven Roller (MDR) Conveyor queueing erected empty cartons toward the case loading station | Integrated low-tape/broken-tape optical sensors and bottom-flap fold verification sensors prior to case release | Automatically erects cartons on demand when Empty Case Queue Low triggers and enters standby when the buffer zone is full |
| Station 3: Cobot Case Packing & Inter-Station Transfer (Pick-and-Place & Conveyors) | Collaborative Robot (Cobot Pick & Place) + Belt & Roller Conveyors + Top/Bottom Case Sealer | Collates verified primary trays, bottles, or pouches into exact layer arrays, picks and places layers gently into erected cartons, and feeds filled cases into the Case Sealer | Dual-lane architecture: FDA PU/PVC Flat Belt (product collation lane) + Roller Conveyor with pneumatic carton clamping stoppers | HIKROBOT Smart Camera OCR verifies 100% of primary date codes + PLC NG Rejector diverts defective packs before the Cobot pick zone | Synchronizes Layer Collation Ready + Empty Carton Clamped interlocks before executing the robot place trajectory |
| Station 4: Secondary Case Coding & Barcode Verification (Closed-Loop Print & Verify) | High-Resolution Case Coder FASTJET TIJ / PIJ (F3500) + HIKROBOT ID Series Barcode Reader | Prints SKU descriptions, lot numbers, and GS1-128 / QR barcodes directly onto corrugated case sidewalls (or via Print & Apply labeler) with immediate inline scan verification | Close-pitch Roller Conveyor (Roller Pitch ≤ 1/3 Shortest Carton Length) or Side-Grip Belt Conveyor with rigid side guide rails | Closed-Loop Verification: Reads 100% of printed case barcodes and checks print contrast; triggers pneumatic pusher diversion into an NG lane if unreadable | Transmits verified case counts to PLC / MES / ERP and triggers an instant line alert if consecutive barcode read failures occur |
| Station 5: Robotic Palletizing & AGV Warehouse Transfer (Robot Palletizer & AGV/AMR) | Robot Palletizer / Cobot Palletizer + Automatic Stretch Wrapper + Autonomous AGV / AMR Fleet | Picks verified shipping cases, rotates and stacks them in interlocking layer patterns onto pallets, wraps the load, and dispatches pallets to warehouse storage via AGV | Zero-Pressure Accumulation Roller Conveyor (infeed buffer) + Heavy-Duty Chain-Driven Pallet Roller Conveyor | Final barcode cross-check against active pallet work orders to prevent mixed-SKU pallet stacking errors | Executes Pallet Full Handshake to summon an AGV/AMR for automated full-pallet pickup and empty-pallet replenishment |
Engineering Deep Dive: Selecting Automatic Carton Erectors & Top Seal Tray Sealers for Jam-Free Continuous Production
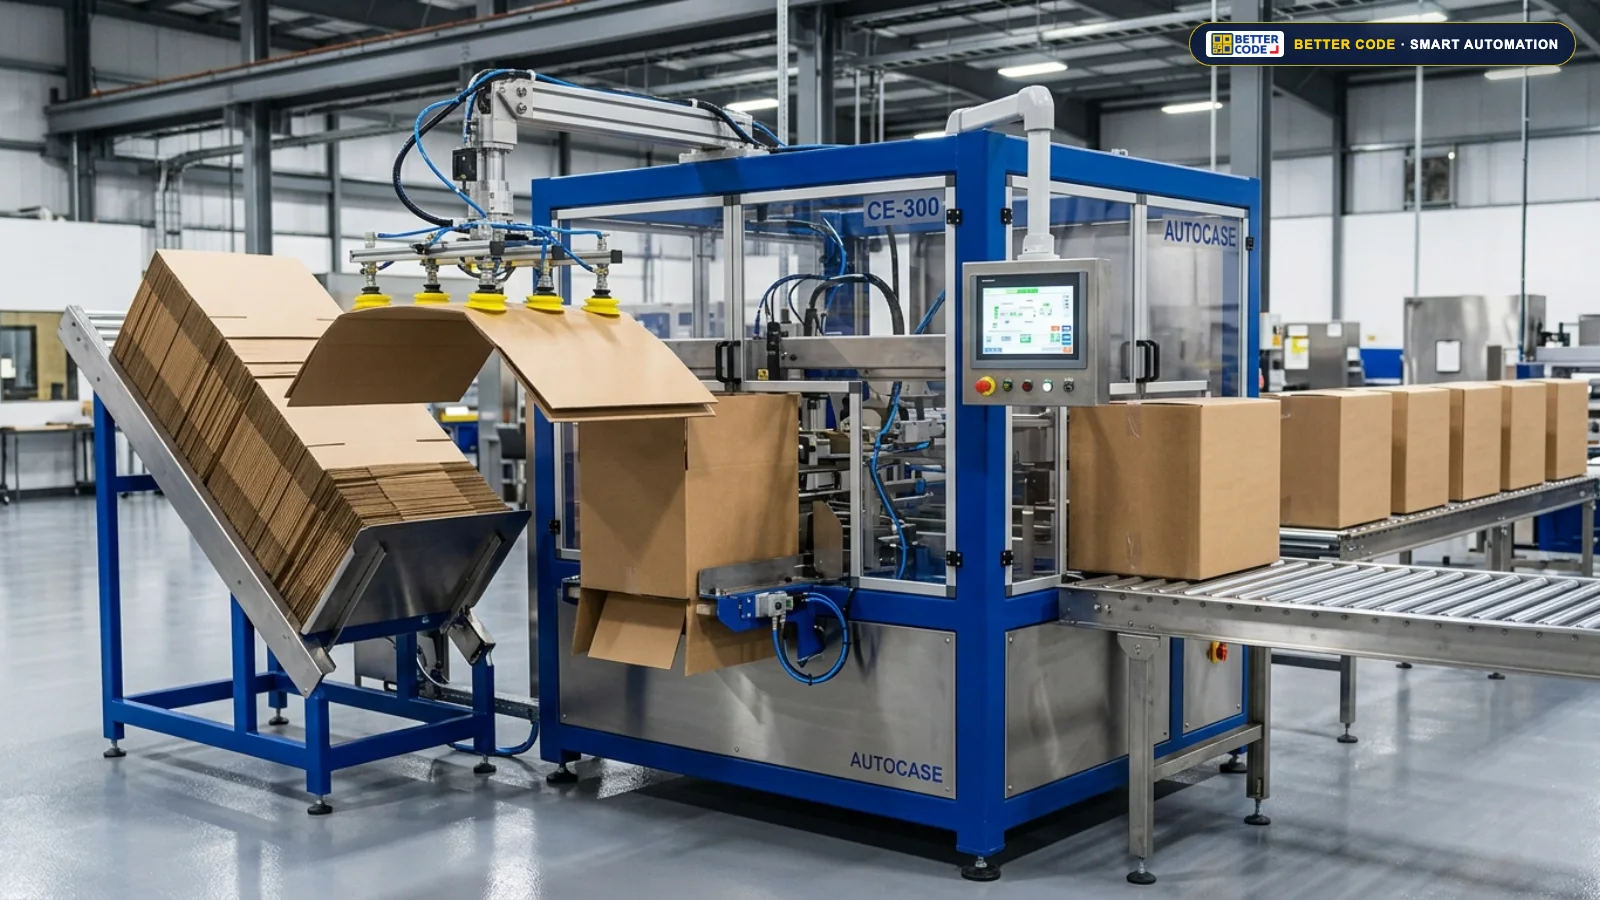
The reliability of an entire End-of-Line Packaging system depends on jam-free primary tray sealing and secondary case forming. Here is how engineers at Better Code Co., Ltd. specify Automatic Carton Erectors (Case Erectors) and Automatic Top Seal Tray Sealers for industrial production lines:
Why Corrugated Boxes Jam in Budget Machines—and How to Specify an Industrial Carton Erector
Understanding what a Case Erector is and why budget machines struggle in humid environments is critical for OEE. In tropical factories, corrugated fiberboard absorbs ambient moisture, softening flute walls and warping blanks stored in magazines—causing single-sided suction arms to drop blanks or fold skewed bottom flaps.
• Dual-Opposing Vacuum Cups & Mechanical Squaring Linkage: Grips adjacent carton panels simultaneously to force a true 90° square opening even on humid, recycled, or slightly warped corrugated blanks.
• Cam-Synchronized Bottom Flap Folding: Folds minor and major flaps smoothly while the case is stationary/guided, eliminating crushed corners before product loading.
• Heavy-Duty OPP Tape Head & Downstream Case Sealer Integration: Spring-loaded wipe-down rollers ensure high-adhesion bottom taping, while leadscrew handwheels with digital counters enable rapid SKU changeovers.
Selecting an Automatic Top Seal Machine: In-Line Continuous vs Rotary & MAP Gas Flushing
For fresh meat, poultry, seafood, ready meals, and cut fruit, upgrading to an Automatic Top Seal Tray Sealer delivers hermetic leak-proof seals, reduces packaging plastic weight compared to snap-on lids, and maximizes retail shelf presentation.
• In-Line Continuous vs Rotary Table: For automated lines connected to infeed/outfeed conveyors and vision inspection, specify an In-Line Automatic Top Seal Machine capable of 15–60+ trays/min straight-through flow.
• MAP (Modified Atmosphere Packaging) Vacuum & Gas Flush: Evacuates residual oxygen inside a sealed chamber and injects food-grade $N_2 / CO_2 / O_2$ gas mixtures prior to heat sealing and precision die-cutting—extending chilled shelf life by 2x to 4x.
• Sanitary SUS304 IP65 Food-Grade Construction: Washdown-ready stainless chassis with quick-change tray tooling and direct mounting brackets for FASTJET film date coders.
Line Balancing & Takt Time Synchronization Formula: Preventing End-of-Line Bottlenecks
The most common engineering mistake when piecing together machines from separate vendors is matching downstream machine speed 1:1 with upstream production. The moment an operator pauses a case sealer to reload tape or waits for a pallet swap, the entire upstream processing line backs up and stops. At Better Code Co., Ltd., we engineer lines using the Line Balancing Formula and accumulation buffers:
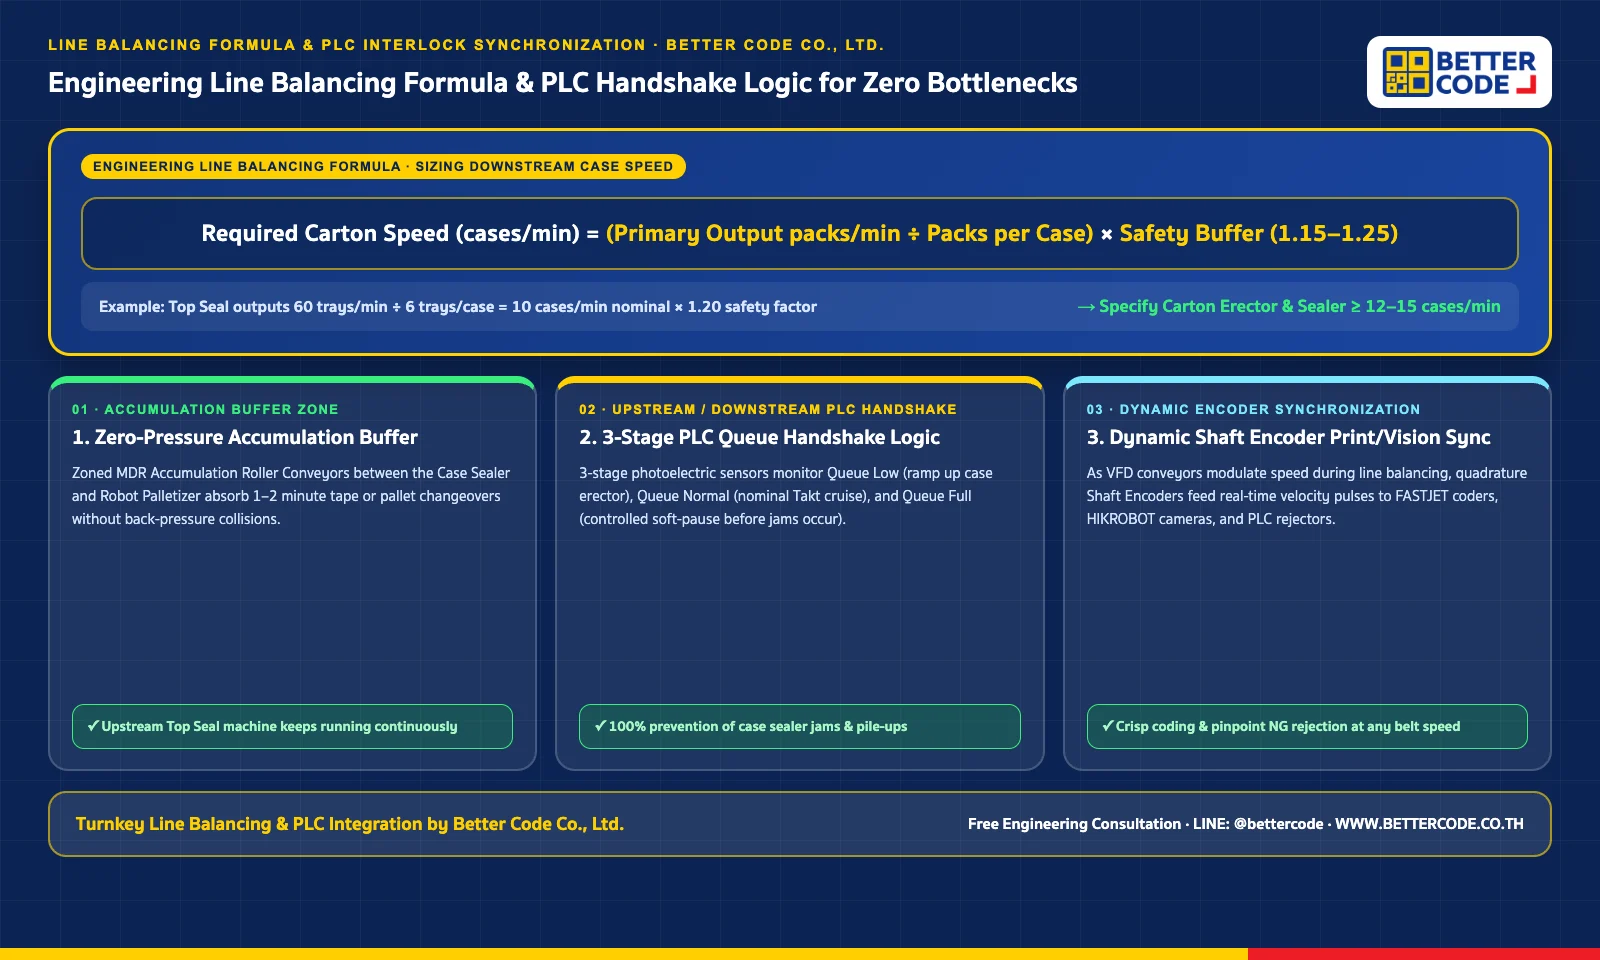
Engineering Formula: Calculating Downstream Case Speed & Safety Buffers (Line Balancing Formula)
To guarantee zero bottlenecks, every downstream station (Carton Erector, Cobot Case Packer, Case Sealer, and Robot Palletizer) must be sized with a 15% to 25% speed safety buffer (1.15–1.25x multiplier) above nominal upstream throughput so buffered queues drain rapidly after minor consumables refills:
Practical Engineering Example: If an upstream Automatic Top Seal Machine outputs 60 trays/min packed at 6 trays per corrugated carton, nominal case flow is 60 ÷ 6 = 10 cases/min. Applying a 1.20 safety factor yields 10 × 1.20 = 12 cases/min (you should specify a Carton Erector, Case Sealer, and barcode inspection station rated for at least 12–15 cases/min).
Technique 1: Installing Zero-Pressure Accumulation Conveyors Between Core Stations
Even with a 20% speed safety buffer, operators occasionally need 60–90 seconds to splice OPP tape rolls or swap pallets. Integrating a zoned Accumulation Roller or Belt Conveyor between the Case Sealer and the Robot Palletizer provides a physical buffer queue—allowing cartons to accumulate cleanly without back-pressure collisions while the upstream Top Seal machine keeps running uninterrupted.
Technique 2: PLC Interlock Handshakes (Upstream / Downstream Queue Control)
Engineers at Better Code Co., Ltd. wire every station into a unified PLC Interlock architecture (Dry Contact I/O, Modbus TCP/IP, or EtherNet/IP) using 3-stage photoelectric queue sensors: Queue Low (ramp up carton erector feed), Queue Normal (cruise at nominal Takt time), and Queue High/Full (execute controlled soft-pause before jams occur).
Technique 3: Real-Time Shaft Encoder Tracking for FASTJET Coders & HIKROBOT Vision
Because VFD-driven conveyors dynamically speed up and slow down during line balancing, fixed-time print delays cause stretched characters and mistimed rejections. We mount quadrature Shaft Encoders directly on conveyor rollers to feed real-time velocity pulses to FASTJET date coders, HIKROBOT barcode & vision cameras, and PLC shift-register rejectors.
Technique 4: Matching Cobot Case Packers vs Industrial Robot Palletizers to Takt Time
For secondary case loading where footprint is tight and operators work alongside equipment, a Collaborative Robot (Cobot) provides cage-free flexibility. At the final palletizing stage—especially when handling heavy cases orhigh-speed multi-line outputs—a high-payload Industrial Robot Palletizer ensures maximum cycle speed and stacking height (see our detailed comparison in the Cobot vs Industrial Robot Palletizer ROI Guide).
Why Ordering Packaging Machinery, Conveyors, Date Coders & Vision Inspection from One Integrator (Better Code Co., Ltd.) Eliminates Multi-Vendor Finger-Pointing 100%
When factories purchase a Carton Erector from Vendor A, conveyors from Vendor B, date coders from Vendor C, and vision cameras from Vendor D, integration gaps inevitably appear during commissioning—and every vendor blames another vendor’s equipment. Partnering with Better Code Co., Ltd. for turnkey Factory Automation solves this across 6 critical engineering pillars:
We custom-fabricate all Belt and Roller Conveyors so pass-line elevations, side guides, and transfer plates match your Top Seal machine, Carton Erector, Case Sealer, and Palletizer down to the millimeter.
Instead of makeshift field brackets, our 3D mechanical design builds vibration-free mounts for FASTJET CIJ, TIJ, and Laser coders, HIKROBOT cameras, shaft encoders, and pneumatic NG rejectors directly into the line chassis.
One automation engineering team writes the entire PLC handshake logic, encoder shift registers, and alarm diagnostics connecting all 5 stations—eliminating communication protocol mismatches.
We test carton erecting, tray sealing, date printing, OCR/barcode scanning, and rejection using your actual corrugated blanks and trays at target Takt speeds prior to site installation.
Start with your highest-ROI bottleneck today (such as an Automatic Carton Erector + Case Sealer + Coding/Vision Conveyor) pre-wired with mechanical and PLC provisions for future Cobot or Robot Palletizer expansion.
From printer inks, ribbons, and vacuum cups to conveyor spares, vision camera recalibration, and new SKU recipes, Better Code Co., Ltd. provides unified nationwide engineering support.
Send your primary tray/pack dimensions, corrugated carton sizes (W×L×H), and target throughput via our Request a Quote page or LINE @bettercode for an on-site engineering survey and turnkey proposal.
Frequently Asked Questions: End-of-Line Packaging, Carton Erectors & Top Seal Machines (FAQ)
What is a Case Erector (Carton Erector) and how does it differ from an Automatic Case Sealer?
An Automatic Carton Erector (Case Erector) operates at the start of secondary packaging: it pulls a flat corrugated blank from a powered magazine, squares the carton at a 90° angle using dual-opposing vacuum frames, folds the four bottom flaps, and applies bottom OPP tape. An Automatic Case Sealer operates downstream after products are loaded into the box—automatically folding the top flaps and sealing both top and bottom seams before case coding and palletizing.
Why do corrugated cartons in tropical climates often jam inside budget carton erectors?
High ambient humidity in Southeast Asian factories causes corrugated board to absorb moisture, softening flute rigidity and warping die-cut score lines. Budget machines that rely on single-sided suction cups often fail to square warped blanks. Better Code specifies industrial Carton Erectors equipped with multi-cup opposing vacuum arms, positive mechanical corner-squaring linkages, and spring-loaded tape wipe-down rollers that handle humid and recycled corrugated cases reliably.
What is the difference between a standard Automatic Top Seal Machine and a MAP (Modified Atmosphere Packaging) Tray Sealer?
A standard inline Automatic Top Seal Machine heat-seals barrier lidding film onto preformed trays (PP, PET, CPET, or pulp trays) and precision die-cuts the film perimeter for leak-proof presentation. A MAP (Modified Atmosphere Packaging) Top Seal system adds a vacuum chamber stage that evacuates oxygen and flushes food-grade protective gas mixtures (such as N2 and CO2) before sealing—inhibiting microbial growth and extending chilled shelf life by 2x to 4x for fresh meat, seafood, and ready meals.
Where should FASTJET date coders and HIKROBOT vision cameras be positioned along an end-of-line packaging system?
For 100% zero-defect compliance, integrate closed-loop verification at two control points: (1) Primary Packaging Station—mount a FASTJET TIJ, CIJ, or Laser coder on the Top Seal film feed or outfeed conveyor paired with a HIKROBOT Smart Camera (OCR/OCV) and pneumatic rejector so no misprinted tray enters a carton; and (2) Secondary Case Station—mount a FASTJET high-resolution case coder after the Case Sealer paired with a HIKROBOT ID Series barcode reader before the Robot Palletizer.
How do we calculate line speeds across stations to prevent end-of-line bottlenecks?
Apply the engineering Line Balancing Formula: Required Carton Erector Speed (cases/min) = (Primary Output in packs/min ÷ Packs per Case) × Safety Buffer (1.15 to 1.25). For example, if a Top Seal machine outputs 60 trays/min packed 6 trays per carton (10 cases/min nominal), specify a Carton Erector and Case Sealer rated for at least 12–13 cases/min and install an Accumulation Roller Conveyor between stations so tape roll changes never halt upstream food sealing.
Does Better Code Co., Ltd. provide turnkey end-of-line packaging design, fabrication, and PLC integration?
Yes. Better Code Co., Ltd. serves as a single-source turnkey integrator—supplying Automatic Top Seal tray sealers, Carton Erectors, Case Sealers, custom Belt and Roller Conveyors, FASTJET date coders, HIKROBOT machine vision systems, Cobot case packers, Robot Palletizers, and AGV/AMR fleet handoffs under unified mechanical pass-line engineering and PLC interlock control.
Consult Our Engineers & Request a Turnkey End-of-Line Packaging Quotation from Better Code Co., Ltd.
Whether you need an standalone Automatic Carton Erector, Case Sealer, or Automatic Top Seal Tray Sealer, or a complete turnkey Factory Automation line uniting custom conveyors, FASTJET date coders, HIKROBOT vision cameras, Cobots, and Robot Palletizers, Better Code Co., Ltd. is ready to survey your plant and deliver an itemized engineering proposal.
Request Turnkey Packaging Quote ↗Explore Turnkey Factory Automation ↗Explore Custom Conveyor Systems ↗Send Line Layout on LINE @bettercode ↗Engineering References & End-of-Line Packaging Design Standards
- End-of-Line Packaging Automation mechanical and control engineering standards (Automatic Carton Erectors, Case Sealers, and Sanitary SUS304 Top Seal / MAP Tray Sealers): Factory Automation Engineering Division, Better Code Co., Ltd.
- Production Line Balancing formulas, Zero-Pressure Accumulation Roller Conveyor buffering, and PLC Upstream/Downstream interlock integration with FASTJET date coders and HIKROBOT machine vision systems.